Modern Computer Numerical Control (CNC) milling centers, automated EDM wire machinery, and precision grinding tool stations rely on compact 12.1-inch operator displays integrated directly into machine console doors. A 12.1-inch 4:3 format display (1024×768 XGA resolution) provides native 1:1 pixel rendering for standard machine tool software, toolpath simulation graphics, and digital readout (DRO) coordinate tables without distorted interpolation. Connected via industrial video extensions to centralized control computers, these satellite touch monitors serve as primary machine control stations.
However, factory machine enclosures expose electronic monitors to severe electrical power fluctuations and electromagnetic noise. When high-power spindle motors and hydraulic pump contactors cycle, inductive energy stored in machine power transformers discharges into the DC bus, generating high-voltage load-dump transients (surpassing 80V on nominal 24V lines). Furthermore, transmitting high-frequency digital DVI video over 15 to 25 meters through crowded cable tracks induces common-mode noise. Maintaining 24/7 reliability across modern industrial skids alongside stainless steel monitor consoles requires analyzing load-dump transient clamping, DVI differential integrity, and preventative maintenance protocols.
1. ISO 7637-2 Inductive Load-Dump Surge Clamping & TVS Diode Physics
When high-power inductive machine components suddenly disconnect, magnetic energy collapse dumps a high-voltage surge into the 24V DC power rail. An industrial wide-voltage power stage utilizes multi-stage Transient Voltage Suppressors (TVS) to clamp this voltage spike safely:
ISO 7637-2 Pulse 5b Transient Clamping & Power Absorption Equation: Unclamped Peak Surge Voltage: V_surge = 87.0 Volts (Nominal 24V bus load dump). Source Internal Impedance: R_source ≈ 2.0 Ω. TVS Diode Breakdown Voltage: V_br = 39.0 Volts; Maximum Clamping Voltage: V_clamp = 48.0 Volts. Peak Surge Discharge Current: I_peak = (V_surge – V_clamp) / R_source = (87.0 – 48.0) / 2.0 = 39.0 / 2.0 = 19.5 Amperes. Peak Dissipated Transient Power: P_peak = V_clamp × I_peak = 48.0 × 19.5 ≈ 936.0 Watts. TVS Component Rating: The onboard primary suppression stage utilizes a 1,500W rated automotive-grade TVS diode array: Safety Margin: P_rated / P_peak = 1,500 / 936 ≈ 1.60 × margin. Circuit Protection: High-voltage surge energy is clamped to 48V within ≤ 1 nanosecond, allowing the internal synchronous buck-boost converter (operating from 9V to 36V) to maintain stable 12V output to the LCD panel without rebooting.
Because the wide-voltage DC power converter absorbs surges up to 1,500 Watts while filtering noise from 9V to 36V DC, the monitor operates continuously through severe machine startup power dips and inductive load-dump spikes without flickering or dropping video sync.
To eliminate electrical surge burnouts and guarantee continuous machining uptime, maintenance engineers standardize on the 12.1″ CNC Panel Mount Touch Monitor (9-36V, DVI) which combines an industrial wide-voltage DC input with a rugged CNC panel-mount aluminum bezel.
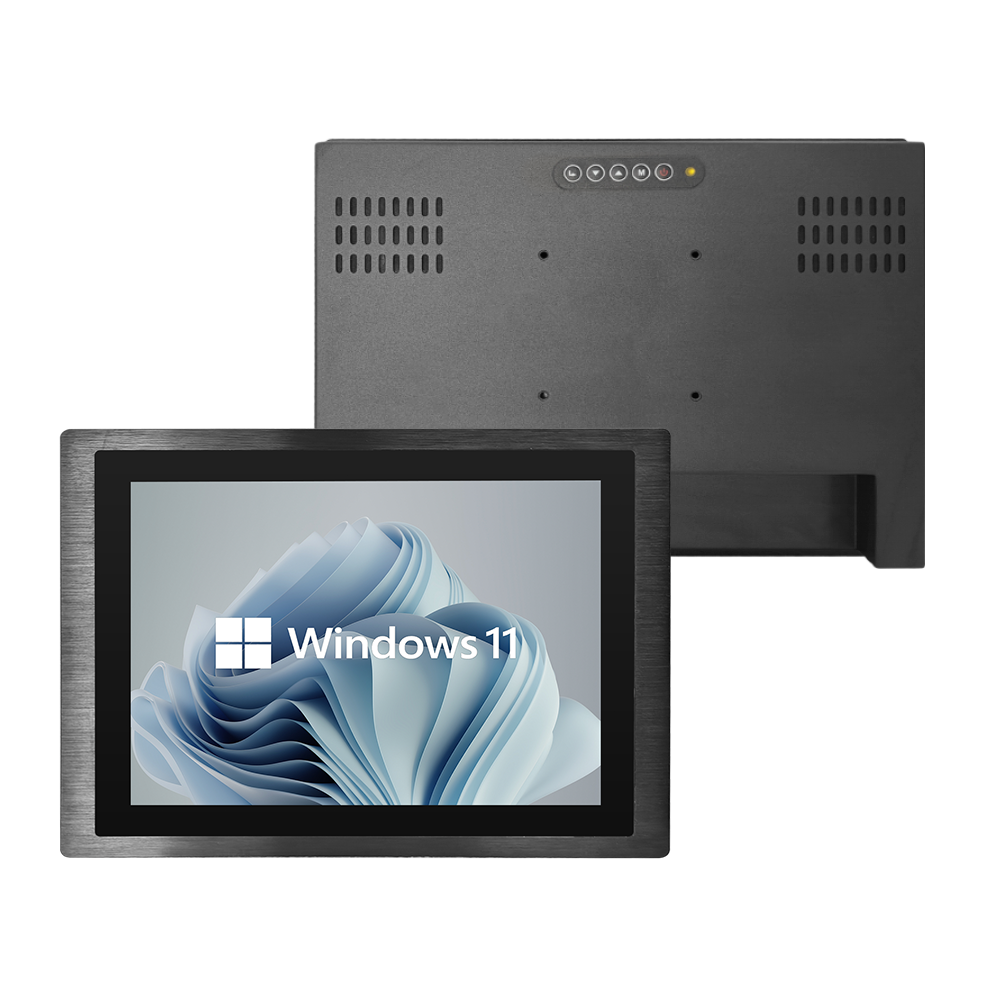
12.1″ CNC Panel Mount Touch Monitor (9-36V)
Designed for CNC machine tool consoles, EDM wire skids, and precision grinding stations. Features a solid 6061 CNC aluminum front bezel, wide DC 9V-36V input with 1500W load-dump surge protection, screw-locking DVI/VGA/HDMI inputs, and IP65 front cutting-oil sealing.
2. DVI Differential Signal Integrity & IP65 Gasket Preload Care
Maintaining high-definition digital video across industrial machine tracks requires disciplined interface care:
- DVI Transition-Minimized Differential Signaling (TMDS): Transmits uncompressed digital video over shielded twisted pairs with hardware clock recovery, resisting electromagnetic interference emitted by adjacent variable frequency drives (VFDs).
- Solid CNC Aluminum Front Frame: Precision-milled from solid 6061 aluminum alloy, the front bezel resists bending under operator touch forces, maintaining uniform 1.0 MPa compression across the closed-cell neoprene perimeter gasket.
- Industrial Multi-Video Inputs (DVI + VGA + HDMI): Features screw-locking thumbscrews on video ports to prevent cables from backing out under continuous machine vibration.
Commercial Monitor vs. Engineered 12.1″ CNC Industrial Monitor
| Diagnostic Checkpoint | Standard Commercial Monitor | INNODA 12.1″ CNC Industrial Monitor |
|---|---|---|
| DC Power Voltage Range | Fixed 12V DC ±5% (Burns out on spikes) | Wide DC 9V to 36V with 1500W TVS surge clamp |
| Video Connector Retention | Friction fit (Shakes loose from vibration) | Screw-locking industrial DVI, VGA, and HDMI |
| Chassis Construction | Molded plastic casing (Degrades in oil) | Solid billet CNC-machined 6061-T6 aluminum |
| Front Ingress Protection | IP50 (Coolant mist penetrates seam) | Certified IP65 dust-tight and cutting-oil sealed |
| Operating Temperature | 0°C to +40°C (Overheats in summer) | -20°C to +70°C fanless wide-temperature design |
3. Scheduled Semi-Annual Preventative Maintenance Checklist
- DC Power Rail Ripple Check: Measure input DC voltage ripple using an oscilloscope during machine motor startups, verifying that peak-to-peak ripple remains under 200 mV.
- DVI Thumbscrew Retorquing: Verify that DVI and VGA thumbscrews maintain 0.4 Nm torque, ensuring continuous 360-degree ground shielding contact against factory EMI.
- Perimeter Gasket Inspection: Inspect the closed-cell neoprene seal around the bezel perimeter for cutting oil embrittlement, re-torquing rear panel clamps to 1.0 Nm to preserve IP65 integrity.
Implementing a routine preventative maintenance protocol for 12.1-inch CNC panel-mount touch monitors eliminates inductive electrical surge failures and ensures lasting video stability. Contact INNODA’s machine automation engineering team to request 3D CAD panel cutout drawings, power wiring schematics, and custom mounting hardware.